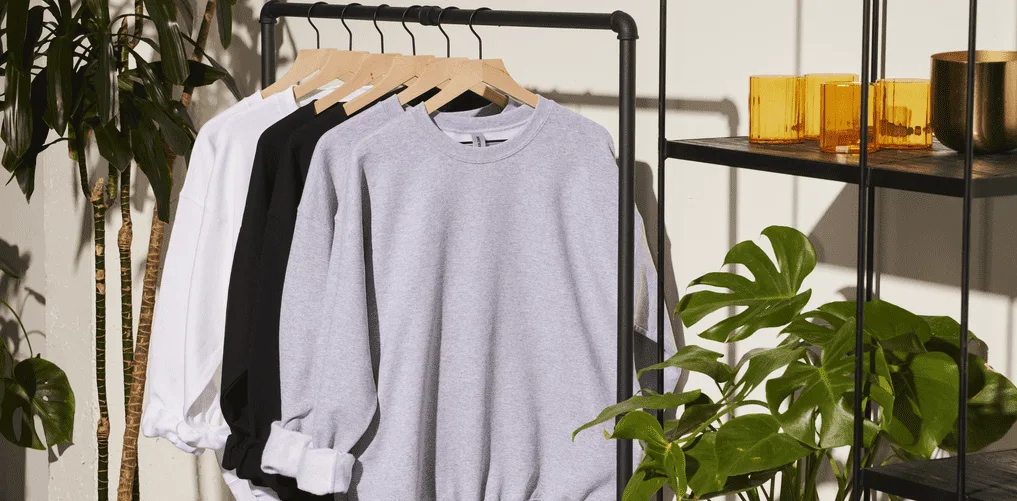
Launching a massive custom merchandise drop or company-wide outfitting project requires clear coordination between graphic designers, production crews, and purchasing teams. When planning large-scale print runs, buyers often focus on the artwork design while overlooking the physical traits of the base textile. Selecting Bulk Orange Sweatshirts for your next production run provides a bold, high-visibility backdrop that demands attention on retail racks, trade show floors, and campus grounds.
Executing a high-volume decorated fleece order without evaluating garment mechanics can quickly lead to production delays, dye bleeding, and disappointed clients. Understanding yarn quality, dye behaviors, and curing requirements ensures that your finished print-ready garments look crisp, feel soft, and stand up to routine washing.
Fabric Mechanics and Print Performance
A commercial print shop relies on consistent fabric construction to produce razor-sharp graphic detail. Fleece is an inherently complex textile because it combines an outer knit face with a brushed, lofty interior.
Matching your preferred decoration style to the fiber blend of the base garment prevents common print flaws like fibrillation, ink cracking, and surface discoloration.
Cotton-Rich Faces vs. Blended Knits
The composition of the garment face determines how ink settles onto the fabric. Standard fifty-fifty cotton-polyester blends offer great pill resistance and low laundry shrinkage, but the synthetic content requires low-cure inks to prevent polyester dyes from gassing out into your top inks.
Blanks featuring an eighty-twenty cotton-polyester blend with a dedicated one hundred percent combed cotton face provide an ideal surface for detailed screen printing and digital direct-to-garment systems. Pure cotton strands absorb liquid ink smoothly, allowing fine detail lines and tight text to cure cleanly without fuzzy fiber migration.
Taking time to verify that your chosen fleece blank has a smooth, tightly knit exterior prevents hours of press calibration issues in the print shop.
The Proven Stability of Gildan Sweatshirts
For large-scale commercial printing jobs that demand predictable sizing and consistent dye lots across hundreds of cartons, decorators routinely turn to proven industry staples. Heavy-blend Gildan Sweatshirts provide the reliable tensile strength and sturdy surface tension required to handle multi-color automatic presses without stretching off-registration.
Their balanced fabric construction holds its shape across high-temperature conveyor dryers, ensuring that graphics cure thoroughly without causing the torso fabric to warp or shrink unevenly.
Choosing an established, time-tested fleece blank protects commercial print shops from costly re-prints and keeps client delivery timelines on schedule.
Technical Considerations for Decorating Saturated Colors
Printing on vibrant, saturated textiles introduces distinct chemical and mechanical challenges that do not exist when printing on neutral white or grey fabrics. Bright orange dyes are reactive and sensitive to excessive dryer heat, requiring disciplined print shop protocols.
Setting up your press runs with proper underbase barriers and calibrated squeegee angles ensures long-lasting graphic brilliance.
Laying Down an Opaque Underbase
Applying light-colored inks like white, pale yellow, or light blue directly onto bright orange fabric results in dull, muddy colors. The heated dye in the fleece fibers rises through the wet ink film during the curing process, tinting the graphic.
Decorators must lay down a solid, flash-cured white underbase screen first. This white layer acts as an opaque physical barrier between the dyed textile fibers and the finished top colors.
Using low-bleed, low-cure plastisol inks allows print operators to cure garments at lower dryer temperatures, stopping dye migration before it starts while keeping the ink deposit flexible and soft against the chest.
Direct-to-Garment and Hybrid Print Challenges
Direct-to-garment (DTG) printing on bright, saturated fleece requires specialized pre-treatment application. Pre-treatment fluid acts as a chemical primer that forces water-based white ink to gel immediately upon hitting the fabric, preventing it from soaking deep into the fleece knit.
Applying too much pre-treatment can leave a visible stain ring around the design, while using too little causes the ink to look washed out after a single home laundry run.
Commercial print shops must test and dial in their pre-treatment sprayers and heat-press curing times before launching high-volume automated digital runs.
Supply Chain Management and Warehouse Sourcing
Managing logistics for a major print campaign requires steady blank availability and transparent shipping tracking. Running out of critical mid-sizes halfway through a production schedule halts automatic presses and ruins client delivery commitments.
Strong wholesale relationships shield print businesses from inventory gaps during peak seasonal runs.
Securing Consistent Case Lots with Simplstc Apparel
Commercial printing businesses need inventory partners who provide real-time stock visibility and dependable freight handling. When suppliers show inaccurate warehouse counts, print shops face frantic garment substitutions and delayed distribution dates.
Working with dependable blank apparel sources like Simplstc Apparel gives print operators and brand managers steady access to first-quality fleece blanks across core size distributions. Sourcing inventory through verified distribution channels via simplstcapparel allows production managers to plan automatic press schedules around verified warehouse counts and predictable transit timelines.
Consistent inventory shipments give your print team the confidence to book large corporate contracts without worrying about inventory gaps.
Incoming Inventory Inspection Protocols
Establishing a clear intake procedure when delivery trucks unload blank inventory prevents expensive shop errors. Once a blank garment runs under an automatic press squeegee or embroidery frame, blank distributors cannot accept it for return.
Unpack sample boxes from each size run to check neck tags, sleeve lengths, and seam stitching before sending garments to the staging tables. Look for needle holes, loose shoulder threads, or irregular collar ribbing that could affect the final product.
Catching rare factory defects before printing starts protects your bottom line and maintains high quality across the entire customer order.
See also: Need Bookkeeping Services for Small Business? Read This!
Structuring Large Orders for Maximum Practical Utility
High-volume apparel orders serve diverse organizational needs, from athletic sidelines and race courses to retail shelves and workforce uniform programs. Designing apparel that recipients genuinely want to wear maximizes the marketing return on every printed piece.
- University club sports and campus organizations that need vibrant spirit wear that stands out in packed stadium bleachers.
- Road race and marathon production teams that outfit marshals, safety crews, and volunteers in high-visibility outerwear.
- Streetwear startups and independent apparel brands that introduce limited-edition seasonal drops with bold back graphics.
- Construction and field service companies that require comfortable mid-layer garments that comply with job-site visibility standards.
Delivering Enduring Quality in Large Print Runs
Succeeding in large-scale garment printing requires balancing artistic vision with practical fabric performance. A brilliant graphic design loses its impact if applied to flimsy fleece that pills or bleeds after two trips through a home washing machine.
By taking time to analyze yarn construction, using proper underbasing techniques, and partnering with dependable blank suppliers, print shops and corporate buyers can execute large apparel orders with complete confidence.
Investing in the right blank base ensures your custom merchandise looks sharp on delivery day and continues promoting your brand across communities for years to come.