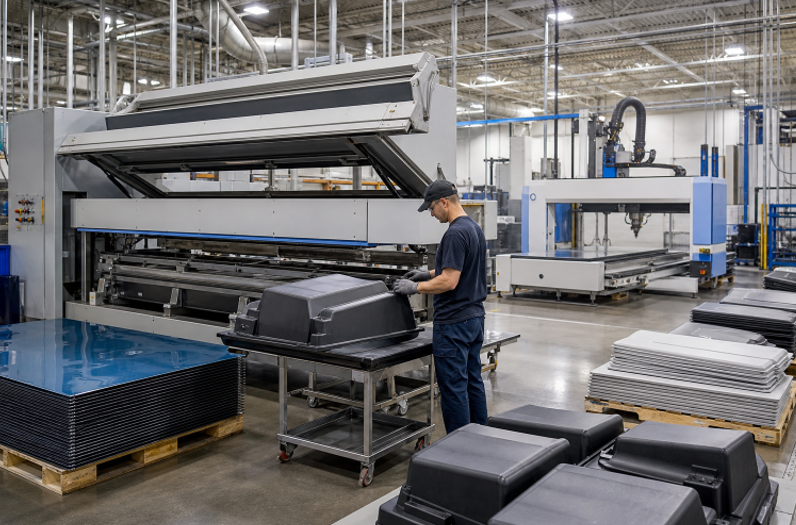
For Kansas product teams, selecting a plastic manufacturing process is not simply a purchasing decision. Parts used in agricultural equipment, industrial machinery, transportation, medical devices, and outdoor installations may be subject to vibration, dust, repeated cleaning, moisture, sunlight, and seasonal temperature changes. The manufacturing method should support the real job the component must perform. When large custom components are under consideration, Plastic Thermoforming from Neodesha Plastics Inc. is a relevant Kansas resource for teams evaluating custom sheet-forming work. Based in Neodesha, Kansas, the company provides engineering support, prototyping, tooling, and production services for applications such as industrial equipment housings, panels, trays, and large covers, making its experience particularly useful to manufacturers that need a path from concept through scalable production in the central United States.
Why Process Choice Matters Early
Process selection affects much more than the unit price. It influences tooling investment, lead time, material use, surface quality, finishing work, inspection methods, packaging, and the cost of future revisions. A large machine cover and a small retaining clip may both be plastic parts, but their manufacturing needs can be entirely different. Reviewing alternatives while the design is still flexible helps teams avoid forcing a part into a process that does not suit its size or intended use.
Start With the Part’s Main Function
Ask one practical question first: What must this part do every day? A protective electronics enclosure may prioritize impact resistance and a sealed fit. A visible equipment panel may prioritize color consistency, texture, and clean edges. A laboratory tray may need a surface that can be cleaned reliably. A bracket may need stiffness, mounting accuracy, and vibration resistance. Function should lead process selection because it determines which material properties, dimensions, finishes, and assembly features actually matter. This is especially important for Kansas manufacturers supporting field equipment or industrial operations, where routine wear can reveal weaknesses that were not obvious in a digital model.
Review Size, Shape, and Detail
Large panels, liners, housings, trays, and protective shells are often practical candidates for sheet-based forming. Smaller components with internal threads, intricate ribs, enclosed features, or highly complex geometry may point toward injection molding or CNC machining instead. During thermoforming, the heated sheet stretches over or into a tool, so deep draws, tight corners, and abrupt transitions require careful planning to maintain usable material thickness.
Part Size, Depth, and Wall Distribution
Large panels, liners, housings, trays, and protective shells are often practical candidates for sheet-based forming. Smaller components with internal threads, intricate ribs, enclosed features, or highly complex geometry may point toward injection molding or CNC machining instead. During thermoforming, the heated sheet stretches over or into a tool, so deep draws, tight corners, and abrupt transitions require careful planning to maintain usable material thickness.
Surface and Assembly Features
Mounting holes, cutouts, logos, textures, trim lines, ribs, and labels should be identified early. Some features can be formed directly, while others are better created through secondary routing, drilling, fastening, printing, or assembly. A basic overview of the thermoforming process outlines the core sequence: heating a plastic sheet, shaping it with a mold, cooling it, and trimming it into a finished part.
Match the Method to Production Volume
Expected volume and design stability should be considered together. At the prototype stage, teams usually value speed, fit checks, and the ability to make changes. For low-volume production, setup labor, tooling expense, and finishing operations may have an outsized effect on cost. At higher volumes, cycle time, automation, tool durability, scrap handling, and repeatability become more important. If demand remains uncertain, a flexible approach may be preferable to committing immediately to the most expensive production tooling.
Compare Thermoforming, Injection Molding, and CNC Machining
- Thermoforming: Often considered for large, lightweight shells, covers, panels, housings, liners, and trays. Teams should plan for material stretch, trim access, and secondary operations.
- Injection molding: Often considered for high-volume parts that need repeatable detail, complex molded features, and consistent part-to-part geometry. It can require substantial upfront tooling development.
- CNC machining: Often considered for prototypes, fixtures, low-volume components, and parts requiring precise cut geometry. Machining time and material removal can become less attractive as size and volume rise.
Many successful projects use more than one method. A team might machine prototype fixtures, thermoform the main enclosure, and use CNC routing to create final openings and mounting locations.
Compare Vacuum Forming and Pressure Forming
Vacuum Forming
Vacuum forming heats a plastic sheet and uses a vacuum to draw it against a mold. It can suit a broad range of shapes, such as protective covers, equipment liners, trays, and housings. Designers should review the draft, corner radii, draw depth, material distribution, and access for trimming before finalizing the tool.
Pressure Forming
Pressure forming combines vacuum with pressurized air to push heated material more tightly into the mold. It can be useful when a part needs sharper visual definition, texture, branded surfaces, or more pronounced details. The thermoforming fundamentals studied by UMass Lowell’s plastics engineering program provide helpful context for teams comparing forming methods and tooling decisions.
Choose Materials by Performance Needs
Material selection should follow the operating environment rather than habit or initial sheet price. Review impact resistance for drops and vibration, temperature exposure during service, resistance to cleaners or industrial fluids, ultraviolet exposure for outdoor parts, and the appearance requirements for visible surfaces. Color, gloss, texture, transparency, decorative films, and flammability or food-contact requirements should be identified before tooling begins. Teams should also discuss whether production scrap can be recovered or recycled within their material and process plan.
Use Design for Manufacturability Before Tooling
- Confirm the material and performance requirements before locking in fine details.
- Review draft angles, radii, deep areas, and possible thinning.
- Define trim lines, holes, mounting points, and assembly interfaces.
- Identify critical dimensions and distinguish them from dimensions that can tolerate variation.
- Use prototypes or sample tools when fit, function, or appearance remains uncertain.
- Maintain clear revision control so that engineering, purchasing, and production use the same design version.
What to Ask a Manufacturing Partner
- Which process best matches the part’s geometry, material, and forecast volume?
- What tooling approach is recommended, and how feasible are future modifications?
- Which trimming, drilling, routing, finishing, assembly, and inspection steps are included?
- How will tolerances, cosmetic requirements, and critical features be measured?
- How will scrap, packaging, freight, and delivery requirements affect total cost?
- Can the supplier support prototype work, pilot runs, and ongoing production?
A Practical Process Selection Checklist
- What will the part experience in its real operating environment?
- How large is it, and which features need the tightest control?
- How many parts are needed before and after launch?
- How likely is the design to change?
- What material, finish, compliance, and durability requirements apply?
- What are the full costs of tooling, finishing, inspection, packaging, and shipping?
See also: Cancel Online Subscriptions Like a Pro: Step-by-Step Tips
Conclusion
No single plastic manufacturing method fits every Kansas project. The best choice comes from evaluating function, geometry, production volume, material performance, tooling, quality expectations, and total cost simultaneously. Teams should also consider factors such as required tolerances, surface finish, part size, production timelines, assembly requirements, and the possibility that the design may change before reaching full production. Injection molding may suit higher-volume parts that justify tooling investment, while other processes may be more appropriate for prototypes, lower volumes, larger components, or specialized geometries. Material selection should be considered alongside the manufacturing process because temperature, chemical exposure, strength, flexibility, and environmental conditions can affect long-term performance. Bringing manufacturing input into the design process early allows engineers and product teams to identify potential production challenges, refine geometry, evaluate tooling requirements, and make more informed material decisions. This early collaboration can reduce avoidable redesigns and create a clearer path to parts that can be produced consistently and work reliably long after the first production run.